We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Choosing Extruded Aluminum Profiles in 2026 requires more than comparing catalog prices. The right profile must balance alloy strength, wall thickness, dimensional tolerance, surface finish, thermal performance, and lifecycle cost. A rail, window frame, robotic guard, or solar mounting channel may look similar on a screen. Its performance can differ significantly in production.
The International Aluminium Institute reported approximately 72 million tonnes of global primary aluminium production in 2024. The U.S. Geological Survey also identified aluminium as a strategically important industrial material, supporting transport, construction, energy, and manufacturing applications. These figures show strong demand, but they do not guarantee that every extrusion is suitable. Design discipline still matters. Sometimes, the cheapest profile creates the most expensive assembly.
Dr. Thomas Sheppard, a recognized aluminium-extrusion researcher and author of Extrusion of Aluminium Alloys, describes extrusion as “a combination of metal forming and heat treatment.” That principle remains useful in 2026. Alloy selection, billet temperature, die design, quenching, and ageing can affect strength and stability before the profile reaches your factory. Buyers should request mill certificates, tolerance data, surface-treatment specifications, and independent test results. Ask about recycled content, too. It may support sustainability goals, but inconsistent feedstock control can affect quality. This is where many purchasing guides become too confident.
This article explains how to compare Extruded Aluminum Profiles using measurable requirements, supplier evidence, and practical application details. Expect trade-offs. There is rarely one perfect profile.
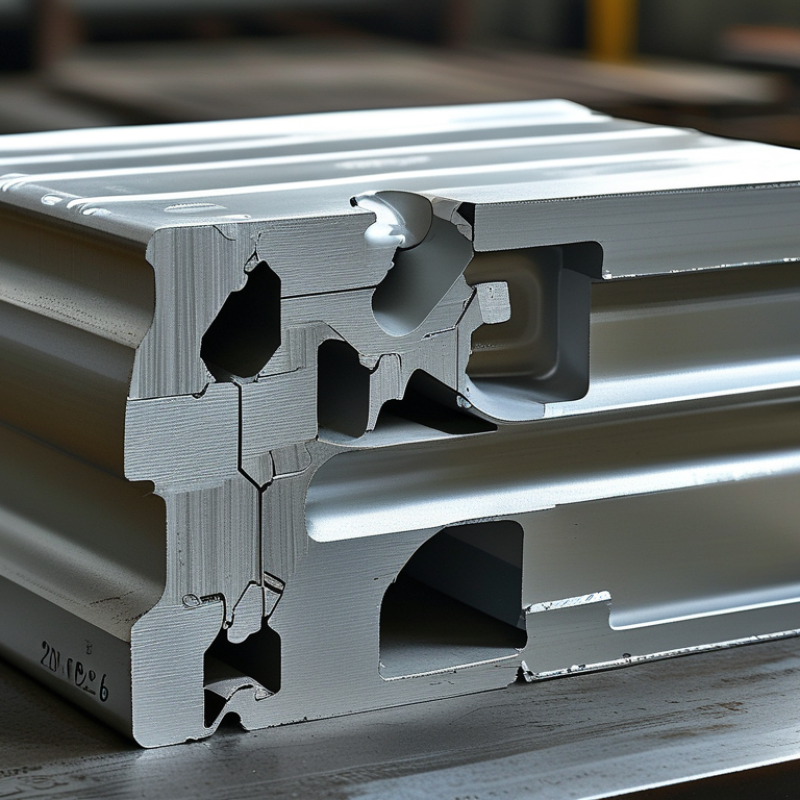
An extruded aluminum profile is a shaped section made by forcing heated aluminum through a steel die. The die creates its final cross-section, such as a channel, tube, rail, or frame member. After extrusion, the profile is cooled, stretched, cut, and heat-treated when required.
The process begins with aluminum billets, often selected by alloy and temper. Alloy 6063 suits clean surfaces and moderate structural needs. Alloy 6061 usually offers greater strength. The choice depends on loads, corrosion exposure, machining, and finishing requirements. During production, technicians check dimensions, straightness, surface marks, and hardness. Small changes in temperature can affect the result.
Choosing a profile in 2026 requires more than comparing price per meter. I check the drawing, wall thickness, load direction, connection method, and expected service environment. For outdoor use, drainage paths and protective finishing deserve attention. Anodizing can improve surface durability, while powder coating offers broader color options. Ask for alloy details, temper information, tolerances, and inspection records. These documents make supplier claims easier to verify. I have seen projects fail because a lightweight profile was selected for a hidden load. It looked efficient. It was not. No profile is perfect. Rechecking assumptions before cutting material can prevent expensive changes later.
Choosing an extruded aluminum profile in 2026 starts with function, not shape. Define load, span, deflection limits, temperature, corrosion exposure, and assembly method. A machine frame needs stiffness and vibration control. An indoor display may need lightness and appearance. Write measurable requirements before requesting a drawing. “Strong enough” is not a specification.
Use calculations for bending, buckling, joint strength, and thermal movement. Do not select by outside dimensions alone. Wall thickness and second moment of area often control performance. The International Aluminium Institute reports that recycled aluminum requires about 5% of the energy used for primary production. Its reports also indicate that roughly 75% of aluminum ever produced remains in use. Therefore, ask about recycled content, alloy, temper, and surface treatment. The lowest initial weight is not always the lowest-impact choice.
Specify tolerances, straightness, finish, inspection methods, and installation access. ISO 6362 provides dimensional and form tolerances for extruded aluminum products. A supplier’s sample is useful, but it is not validation. I have seen a polished profile fail because fasteners weakened its thin wall. That mistake was avoidable. Leave room for drainage, cleaning, replacement, and thermal expansion. My first designs sometimes looked perfect on paper. They were not always practical in a workshop. Recheck the drawing against real tools, hands, and maintenance time.
How to Choose Extruded Aluminum Profiles in 2026?
Selecting the right aluminum alloy and temper starts with the profile’s working conditions. Alloy 6063 is often suitable for frames, rails, and visible architectural sections. It offers smooth extrusion and a clean surface finish. Alloy 6061 usually provides higher strength for machinery supports and load-bearing components. However, stronger is not always better. It may require more careful machining and can increase production costs.
Temper changes the alloy’s performance. T5 profiles are cooled after extrusion and artificially aged. They can provide practical strength for general structures. T6 temper usually delivers higher strength through solution heat treatment and artificial aging. This choice may affect dimensional stability, bending, and cutting behavior. Ask for verified mechanical data, not only a temper label. Real performance depends on section thickness and processing quality.
Tips: Match the temper to the actual load, not the maximum possible load. Check yield strength, corrosion exposure, surface requirements, and joining methods together. Request mill certificates and test results from a qualified supplier. A small sample profile can reveal warping, finish issues, or difficult machining before full production. I have seen designs over-specified for safety, yet still weakened by poor joints. That detail deserves review.
Selecting the Right Aluminum Alloy and Temper
The chart compares typical minimum yield-strength levels for commonly used extruded aluminum alloys and tempers. Higher-strength tempers such as 6061-T6 and 6082-T6 are suitable for load-bearing applications, while 6060-T5 and 6063-T5 are often selected for lightweight architectural profiles, surface finishing, and complex shapes. Actual mechanical values vary by product standard, section thickness, and profile geometry.
How to Choose Extruded Aluminum Profiles in 2026?
Choosing an extruded aluminum profile starts with the drawing, not the finish. Check width, height, wall thickness, hole position, and cutting length. A two-millimeter error can affect brackets, glazing, or automated assembly. Measure the mating parts before requesting quotations. I have seen projects fail because the profile matched the catalog, but not the actual connector.
Compare tolerances against the profile’s function. General frames may accept wider dimensional variation, while sliding tracks and heat sinks need tighter control. Ask for the applicable extrusion standard, inspection method, and measurement records. Do not judge quality from a sample alone. Check straightness, twist, corner radius, and surface marks under realistic lighting. Anodizing gives a durable oxide layer, while powder coating offers wider color choices and stronger visual coverage. Specify coating thickness, color tolerance, gloss level, and adhesion testing. Surface treatment can hide minor defects, but it cannot repair poor extrusion.
Tips: Request a full tolerance table and a cut sample. Compare finished dimensions, not only raw profiles. Confirm whether protection film is required during transport. Ask how the supplier handles batch-to-batch color differences. Keep one approved sample for production checks. Small details matter.
One practical warning: tighter tolerances usually increase cost and may reduce extrusion efficiency. Specify only what the assembly truly needs. Recheck the design after finishing, because coatings can change fit. That step is easy to overlook.
| Comparison Dimension | Common Option or Range | Typical Technical Data | What to Compare | Recommended Selection Guidance |
|---|---|---|---|---|
| Alloy and Temper | 6063-T5 / 6063-T6 | Good extrudability, smooth appearance, and adequate corrosion resistance. Typical tensile strength is approximately 150–240 MPa, depending on temper and product specification. | Strength, surface quality, machinability, corrosion resistance, and availability. | Use 6063 for architectural profiles, frames, trims, and visible surfaces where appearance and extrusion quality are important. |
| Alloy and Temper | 6061-T6 | Higher structural strength than 6063. Typical tensile strength is approximately 260–310 MPa, depending on product form and applicable standard. | Load capacity, weldability, machinability, and heat-treatment requirements. | Choose 6061-T6 for brackets, supports, machine frames, and other applications requiring higher mechanical strength. |
| Profile Width and Height | Approximately 10–300 mm for many standard commercial profiles | Large or complex cross-sections generally require larger presses, more complex dies, and additional dimensional review. | Envelope size, die feasibility, straightness, weight per metre, and assembly clearance. | Keep the cross-section as compact and symmetrical as practical to reduce distortion and control production cost. |
| Wall Thickness | Approximately 0.8–6.0 mm for many general-purpose profiles | Very thin walls are more sensitive to die wear, local distortion, bow, twist, and surface variation. Structural sections commonly use thicker load-bearing walls. | Minimum wall thickness, unsupported length, local stress, screw engagement, and machining allowance. | Use thicker walls around fasteners and load points. Do not specify a minimum thickness without confirming alloy, cross-section, and extrusion capability. |
| Length | Common commercial cut lengths: approximately 1–6 m | Standard extrusion lengths may be supplied longer and cut to order. Cut-length tolerances depend on saw equipment and specified length. | Required finished length, cutting tolerance, end squareness, packaging, and transport limitations. | Define finished length and cut tolerance separately from the extrusion straightness requirement. |
| Dimensional Tolerance | Standard extrusion tolerance versus precision tolerance | Typical profile dimensions may be controlled to about ±0.15–±0.50 mm, but the actual value depends strongly on dimension, wall thickness, alloy, shape, and governing standard. | Critical dimensions, datum references, hole locations, wall thickness, and measurement method. | Reference an applicable standard such as EN 755-9 or ASTM B221 and specify tighter tolerances only for functional features. |
| Straightness | Controlled by bow over a defined inspection length | A commonly used commercial target is approximately 1–2 mm of deviation per metre, subject to profile geometry and the specified standard. | Overall bow, local bow, profile length, inspection surface, and correction method. | Set a measurable bow limit for long frames, sliding components, guide rails, and parts that must align during assembly. |
| Twist | Specified as angular or dimensional deviation along the profile | Thin, asymmetric, and open profiles are generally more susceptible to twist than compact, symmetrical profiles. | Cross-section symmetry, mating surfaces, assembly datum, and acceptable rotational deviation. | Include a twist limit when the profile must connect to panels, seals, bearings, or precision machined components. |
| Surface Finish: Mill Finish | As-extruded aluminum surface | No additional coating. The appearance may include normal extrusion die lines, minor shade variation, and handling marks within the agreed acceptance criteria. | Visual uniformity, die lines, scratches, stains, storage protection, and allowable cosmetic defects. | Use for concealed parts, machined components, or applications where a decorative surface is not required. |
| Surface Finish: Anodizing | Clear, bronze, black, or other electrolytic colors | Typical anodic coating thickness is approximately 10–25 µm. Anodizing improves surface hardness and corrosion resistance but does not remove extrusion marks. | Coating thickness, color tolerance, gloss, sealing quality, corrosion environment, and visible-face requirements. | Specify the anodizing class or thickness, color acceptance sample, and whether the requirement applies to all surfaces or visible surfaces only. |
| Surface Finish: Powder Coating | Polyester powder coating in a selected color and gloss level | Typical dry-film thickness is approximately 60–120 µm, depending on the coating system, geometry, and specification. | Film thickness, adhesion, impact resistance, gloss, color difference, pretreatment, and UV exposure. | Use a qualified architectural or industrial coating specification and define acceptable color and gloss variation before production. |
| Surface Finish: Liquid Paint | Fluoropolymer or other liquid-applied coating systems | Coating thickness varies by system and may be applied in multiple layers. Performance depends on pretreatment, primer, topcoat, and curing. | Primer and topcoat system, dry-film thickness, adhesion, weathering, chemical resistance, and repair procedure. | Choose when high weatherability, a specific appearance, or field-repair compatibility is more important than the simpler powder-coating process. |
| Mechanical Surface Treatment | Brushing, polishing, blasting, or tumbling | These processes alter texture and reflectivity but do not provide the same protective barrier as anodizing or paint. | Surface roughness, directionality, reflectivity, edge treatment, and consistency between batches. | Combine mechanical finishing with anodizing when both a decorative texture and improved surface protection are required. |
| Machining Allowance | Post-extrusion drilling, milling, cutting, or CNC machining | Allowance depends on the required final dimension, profile tolerance, distortion risk, and amount of material to be removed. | Reference datums, flatness, hole position, burr control, coating removal zones, and final inspection method. | Identify all machined features on a drawing and avoid relying on an untreated extrusion surface as a precision datum. |
| Corrosion Environment | Indoor, outdoor, coastal, industrial, or chemically exposed service | Aluminum naturally forms an oxide film, but aggressive chloride, acidic, or alkaline environments can cause localized corrosion. | Exposure to salt spray, humidity, chemicals, galvanic contact, drainage, and coating system durability. | For coastal or industrial exposure, specify suitable pretreatment and coating thickness, isolate dissimilar metals, and prevent water retention. |
| Inspection and Acceptance | Dimensional, visual, coating, and mechanical inspection | Inspection should be based on approved drawings, samples, defined lighting, calibrated instruments, and the selected material or coating standard. | Sampling plan, measurement points, visual distance, inspection lighting, certificates, and nonconformance rules. | Approve a pre-production sample and document critical dimensions, color limits, surface defects, and test requirements before mass production. |
| Note: The numerical ranges above are typical design and purchasing references, not universal acceptance limits. Final requirements should be confirmed against the selected alloy, temper, profile geometry, extrusion capability, surface-treatment specification, and applicable standard. For critical applications, use a controlled engineering drawing with explicit tolerances and inspection methods. | ||||
How to Choose Extruded Aluminum Profiles in 2026?
Supplier evaluation should begin with evidence, not polished samples. Request alloy certificates, temper records, dimensional reports, and traceable batch numbers. ASTM B221 provides a useful reference for aluminum extrusions. ISO 9001 certification also indicates controlled processes, but it does not guarantee perfect products. A supplier should explain die design, minimum order quantities, tooling fees, and production capacity. The lowest quotation often excludes anodizing, machining, packaging, or freight.
Cost needs a longer view. The International Aluminium Institute reports that recycled aluminum uses about 5% of the energy required for primary aluminum production. Ask about recycled content and material origin. Then compare surface treatment thickness, rejection rates, delivery stability, and replacement costs. A profile that saves 8% today may create expensive assembly problems later. This happens more often than purchasing teams admit.
Tips: Order a small pilot batch before signing a long contract. Measure wall thickness at several points. Check corner radii with calipers. Test coating adhesion after cutting and drilling. For outdoor use, request corrosion data and confirm drainage details. During evaluation, I would also inspect packaging; scratched profiles reveal weak handling controls. A perfect sample can still mislead. Review performance after thermal cycles, vibration, and repeated assembly. That step is sometimes skipped. It should not be.
We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Do you consent to the use of ALL cookies?
901 2nd Court West
Birmingham, AL 35204
Sales: 866.481.4036
Logistics/Ops: 866.481.4036
2101 Dralle Road
University Park, IL 60466
Sales: 708.813.9070
Logistics/Ops: 708.235.4200
400 E. 13th Street
Little Rock, AR 72114
Sales: 866.760.5344
Logistics/Ops: 866.760.5344
225 Collins Road
Elkhart, IN 46515
Sales: 574.295.0214
Logistics/Ops: 574.607.4611
601 Berryman Pike
Tipton, IN 46072
Sales: 800.897.7591
Logistics/Ops: 800.897.7591
3900 Uvalda Street
Denver, CO 80239
Sales: 303.706.8000
Ops/Logistics: 303.576.8398
510 3rd Street E
Milan, IL 61264
Sales: 800.322.1052
Logistics/Ops: 800.322.1052
1660 E. Aurora
Des Moines, IA 50313
Sales: 800.671.1660
Logistics: 800.671.1660
86554 Gene Lasserre Blvd.
Yulee, FL 32097
Sales: 904.253.3060
Logistics/Ops: 904.225.3000
694 S.E. County Road 245
Lake City, FL 32025
Sales: 800.727.6706
Logistics/Ops: 386.752.7412
210 Neptune Road
Auburndale, FL 33823
Sales: 863.967.1131
Logistics/Ops: 863.777.9814
4601 McCoy Drive
Pensacola, FL 32503
Sales: 850.308.7030
Logistics/Ops: 850.434.5502
815 South 56th Street
Tampa, FL 33619
Sales: 813.302.1940
Logistics/Ops: 813.621.1352
200 Hosea Road
Lawrenceville, GA 30046
Sales: 770.953.7575
Logistics/Ops: 770.513.6000
Branch Product Guide
Branch Line Card
Moulding Offering
Cedar Offering
Column Offering
8173 Hwy. 165 North
Monroe, LA 71211
Sales: 800.256.4165
Logistics/Ops: 800.256.4165
508 Warren Avenue
Portland, ME 04103
Sales: 207.888.2331
Logistics/Ops: 207.797.6565
4300 Georgia Pacific Blvd.
Frederick, MD 21704
Sales: 301.798.7474
Logistics/Ops: 301.874.8000
419 Maple Street
Bellingham, MA 02019
Sales: 508.449.0535
Logistics/Ops: 508.966.5500
825 Buchanan Ave SW
Grand Rapids, MI 49507
Sales: 877.800.1180
Logistics/Ops: 616.278.0909
995 Pacific St. NW
Aitkin, MN 56431
Sales: 800.432.3727
Logistics/Ops: 218.212.7770
1102 Port Terminal Drive
Duluth, MN 55802
Sales: 800.951.9899
Logistics/Ops: 800.851.9899
9110 83rd Ave. North
Brooklyn Park, MN 55445
Sales: 763.425.0204
Logistics/Ops: 763.425.0204
910 E. Railroad Street
Long Beach, MS 39560
Sales: 866.535.4135
Logistics/Ops: 228.205.2400
1727 Warren Street
North Kansas City, MO 64116
Sales: 800.621.2611
Logistics/Ops: 800.621.2611
2123 North Golden
Springfield, MO 65803
Sales: 800.375.7891
Logistics/Ops: 800.375.7891
13860 Corp. Woods Trail
Bridgeton, MO 63044
Sales: 314.209.0800
Logistics/Ops: 314.209.0800
1109 South 19th Street
Omaha, NE 68108
Sales: 800.489.6637
Logistics/Ops: 800.489.6637
1 Luger Road
Denville, NJ 07834
Sales: 973-339-3539
Logistics/Ops: 973.625.1461
3720 Jeffrey Blvd.
Blasdell, NY 14219
Sales: 716.235.5989
Logistics/Ops: 716.825.6557
319 Yaphank Ave.
Yaphank, NY 11980
Sales: 631.358.5714
Logistics/Ops: 631.924.7401
3300 Parkside Drive
Charlotte, NC 28208
Sales: 800.839.2588
Logistics/Ops: 704.394.3172
1712 East D Street
Butner, NC 27509
Sales: 984.389.8200
Logistics/Ops: 919.575.3700
128 Foothills Drive
Statesville, NC 28687
Sales: 800.222.1414
Logistics/Ops: 704.394.3172
550 Munroe Falls Rd.
Tallmadge, OH 44278
Sales: 330.357.4506
Logistics/Ops: 330.794.1141
10347 Toebben Dr.
Independence, KY 41051
Sales: 859.298.3926
Logistics/Ops: 859.746.2250
450 N. MacArthur
Oklahoma City, OK 73127
Sales: 800.375.6025
Logistics/Ops: 800.375.6025
1680 North Aspen
Broken Arrow, OK 74012
Sales: 918.272.2212
Logistics/Ops: 918.272.2212
522 Bridge Street
Hunker, PA 15639
Sales: 878.217.2001
Logistics/Ops: 724.925.7285
4290 Atlanta Street
Charleston, SC 29418
Sales: 843.371.1420
Logistics/Ops: 843.554.8192
1040 S. Industrial Dr.
Erwin, TN 37650
Sales: 423.641.1005
Logistics/Ops: 423.742.5911
4287 Pilot Drive
Memphis, TN 38118
Sales: 901.365.2101
Logistics/Ops: 901.365.2101
700 Myatt Drive
Madison, TN 37115
Sales: 615.327.9547
Logistics/Ops: 629.777.4949
4747 Mark IV Parkway
Fort Worth, TX 76106
Sales: 866.323.5117
Logistics/Ops: 817.625.9091
6990 Market Avenue
El Paso, TX 79915
Sales: 915.778.6356
Logistics/Ops: 915.265.7200
2502 Wilson Road
Harlingen, TX 78552
Sales: 800.580.6711
Logistics/Ops: 800.580.6711
10,000 North Loop East
Houston, TX 77029
Sales: 713.921.1977
Logistics/Ops: 713.675.3544
702 East 44th St.
Lubbock, TX 79404
Sales: 866.454.6010
Logistics/Ops: 866.454.6010
535 N. WW White Road
San Antonio, TX 78219
Sales: 800.284.0488
Logistics/Ops: 210.333.8112
142 Pine Haven Shores Rd.
Shelburne, VT 05482
Sales: 802.800.2540
Logistics/Ops: 802.985.2512
4700 Bethlehem Road,
Richmond, VA 23230
Sales: 804.201.2400
Logistics/Ops: 804.342.1161
4516 N Barker Road
Spokane Valley, WA 99027
Phone: 509.892.9420
Toll free: 800.728.6157
8365 N. 76th Street
Milwaukee, WI 53223
Sales: 800.356.9245
Logistics/Ops: 800.356.9245
312 S. Chester Street
Sparta, WI 54656
Sales: 800.362.5864
Logistics/Ops: 800.362.5864
899 Grossman Drive
Schofield, WI 54476
Sales: 800.472.0017
Logistics/Ops: 800.472.0017
