We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
A Cleanroom Dehumidifier is more than a cooling accessory. It regulates moisture before humidity damages products, disrupts airflow, or supports microbial growth. In a pharmaceutical cleanroom, that control may protect powder stability, sterile packaging, and operator comfort. The air must feel dry, but not harsh.
The International Organization for Standardization defines cleanrooms through controlled airborne contamination, temperature, humidity, and pressure conditions. ISO 14644-1 focuses on particle classification, while ISO 14644-4 addresses design and operation. Humidity still matters. ASHRAE’s 2023 Handbook—HVAC Applications explains that dehumidification supports stable environmental conditions and reduces condensation risks. Market research also signals strong demand. Grand View Research valued the global cleanroom technology market at approximately USD 5.4 billion in 2023, with pharmaceutical and semiconductor production driving expansion. These figures describe the wider market, not dehumidifiers alone. That distinction deserves attention.
Cleanroom microbiology expert Tim Sandle states, “Cleanrooms are controlled environments designed to minimize contamination.” His point explains the equipment’s purpose. A Cleanroom Dehumidifier removes water vapor from incoming or recirculated air. It commonly uses a chilled coil, desiccant wheel, or hybrid system. The selected method depends on dew point, airflow, heat load, and required cleanliness. For example, a desiccant unit can keep moisture low when chilled coils become inefficient. Yet lower humidity is not automatically safer. Excessively dry air may increase static electricity and handling problems. Engineers must verify performance with calibrated sensors, trend logs, and room-level testing. The equipment can fail quietly. A wet filter, blocked drain, or drifting sensor may reveal the weakness first. Good design is precise, but never careless.
A cleanroom dehumidifier is an air-treatment system designed to remove moisture before air enters a controlled production area. Its purpose is precise: maintain a stable dew point, protect sensitive materials, and reduce moisture-related contamination risks. Unlike a standard commercial unit, it works with filtration, airflow, pressure, and temperature controls. The system usually cools air below its dew point, collects condensate, then reheats the dried air when necessary. Some facilities use desiccant technology for very low humidity requirements.
Humidity control supports cleanliness, but it does not replace particle control. ISO 14644-1:2015 classifies cleanrooms by airborne particle concentration, not relative humidity. This distinction matters. A room can meet its particle class while still suffering condensation, corrosion, static electricity, or unstable processes. The ASHRAE Handbook—HVAC Applications identifies moisture control as a key part of environmental control in sensitive facilities. The U.S. EPA also reports that indoor relative humidity above 60% encourages mold growth, although cleanrooms often require tighter limits. In practice, many pharmaceutical and electronics areas operate around 30% to 50% relative humidity, depending on process needs. Not every room needs the same target. That assumption can waste energy. Engineers should verify dew point, product sensitivity, recovery time, and seasonal load during commissioning. Small errors matter. A poorly located sensor may report comfortable air while moisture accumulates near a cold surface.
A cleanroom dehumidifier controls moisture without compromising the room’s particle-control strategy. Its main components include an intake filter, supply fan, cooling coil, condensate drain, sensors, and a control panel. Some systems also use a desiccant rotor for very low humidity levels. The filter protects internal surfaces. The fan moves air through each treatment stage. Sensors monitor temperature and relative humidity continuously.
Cooling-based units remove moisture by lowering air below its dew point. Water vapor then condenses on the cold coil and flows into a drain pan. The drier air may need reheating before entering the cleanroom. This prevents cold, unstable airflow around sensitive processes. Desiccant systems work differently. A moisture-attracting wheel captures vapor from the process air. Heated regeneration air then releases that moisture outdoors.
Control accuracy matters.
A reliable system responds gradually to changing loads, door openings, and personnel movement. In my experience, humidity readings can drift when sensors are poorly positioned or calibrated too rarely. A sensor near a supply diffuser may not represent room conditions. That detail is easy to miss. Operators should check dew point, coil cleanliness, drain performance, and alarm history during routine inspections. HEPA filtration removes particles, but it does not replace dehumidification. Some designs also waste energy through excessive reheating. The best setup balances moisture control, airflow stability, maintenance access, and verified room performance. Yet even a well-designed unit can underperform when the building envelope leaks humid air.
What Is a Cleanroom Dehumidifier and How Does It Work?
A cleanroom dehumidifier controls humidity through measurement, cooling, drying, and verification. A calibrated sensor reads relative humidity near the production zone. The controller compares that reading with the process target. This target must come from product requirements, not guesswork. ISO 14644-1 classifies airborne particles, but it does not prescribe one universal humidity level.
The air then passes through a cooling coil. Moisture condenses on the cold surface and drains away. If the room needs very dry air, a desiccant wheel removes remaining vapor. The dried air may feel too cold, so a reheat coil restores the supply temperature. Fans deliver this air through terminal filters and maintain the required airflow pattern. Small changes matter.
Operators check supply air, return air, room pressure, and dew point. ASHRAE Handbook guidance links moisture control with corrosion, microbial growth, and static risks. The U.S. Department of Energy reports that HVAC can represent about 40% of commercial building energy use, making over-drying expensive. Cleanrooms may consume 15–50 times more energy per square meter than offices, according to Lawrence Berkeley National Laboratory research. A 45% RH display can still mislead if the sensor drifts, the door opens repeatedly, or cold surfaces create hidden condensation. Good control requires calibration records, alarm testing, and human judgment.
A cleanroom dehumidifier controls moisture before it harms products, equipment, or process stability. It usually cools return air below its dew point, removes condensed water, then reheats the air. Desiccant systems can remove moisture without excessive cooling. This matters in pharmaceutical filling, semiconductor fabrication, medical-device assembly, and dry-powder processing.
Environmental requirements depend on the process, not one universal setting. ASHRAE Standard 170-2021 commonly identifies 30–60% relative humidity for many healthcare spaces, but controlled manufacturing areas may require narrower limits. ISO 14644-1:2015 classifies cleanrooms by airborne particle concentration, not humidity. Therefore, particle compliance alone does not prove moisture control. That assumption is incomplete.
High humidity can support corrosion, microbial growth, condensation, and powder clumping. Low humidity can increase static electricity and damage sensitive materials. A practical system monitors supply-air dew point, room humidity, pressure, temperature, and filter performance continuously. ASHRAE Handbook—HVAC Applications recommends evaluating moisture loads from people, infiltration, equipment, and cleaning processes. Door openings matter. So does wet cleaning. Engineers should verify sensors against calibrated references and review trend data during seasonal changes. In real facilities, the setpoint may look correct while hidden moisture enters through loading doors. This is where commissioning can become imperfect, and routine review remains necessary.
| Data Dimension | Cleanroom Dehumidifier or Environmental Requirement | Typical Design Data or Range | How It Works or Why It Matters | Recommended Control and Verification Method |
|---|---|---|---|---|
| Definition | Cleanroom dehumidifier | Dedicated equipment used to reduce and control moisture in supply air or room air. | It removes water vapor so that relative humidity, dew point, product stability, and process conditions remain within specified limits. | Specify the required moisture-removal capacity, leaving-air dew point, airflow, filtration level, and construction materials. |
| Operating principle | Desiccant dehumidification | Moisture is adsorbed by a rotating or stationary desiccant material and removed during a separate regeneration cycle. | Desiccant systems can produce low dew points and are useful when moisture control is required below the practical range of standard cooling coils. | Verify supply-air dew point under design load and confirm regeneration temperature, energy use, and control stability. |
| Operating principle | Cooling-coil dehumidification | Air is cooled below its dew point so that water vapor condenses on the coil surface. | The condensate is collected and drained from the air stream. This method is commonly integrated into air-handling systems. | Check coil temperature, condensate drainage, reheat requirements, coil cleanliness, and downstream relative humidity. |
| Operating principle | Hybrid dehumidification | Combines cooling-based moisture removal with desiccant drying or heat recovery. | The cooling stage removes a large portion of the moisture load, while the desiccant stage provides a lower dew point or finer control. | Use staged control based on dew point, humidity load, production schedule, and energy-consumption limits. |
| Humidity control | Relative humidity | Common design targets may range from approximately 30% to 60% RH, depending on the process and materials. | Relative humidity affects static generation, corrosion, microbial growth risk, powder behavior, material stability, and operator comfort. | Set the range according to the validated process requirement rather than using a universal value. Measure with calibrated humidity sensors. |
| Humidity control | Low-dew-point operation | Specialized processes may require supply-air dew points below 0°C, with some applications requiring approximately −20°C to −40°C or lower. | Low dew points limit the amount of moisture available to sensitive products and processes, particularly in moisture-controlled manufacturing. | Use dew-point sensors and verify performance at the room connection point, not only at the dehumidifier outlet. |
| Temperature control | Room temperature | A common controlled-room range is approximately 18°C to 24°C, although the validated process range may differ. | Temperature influences relative humidity, process repeatability, equipment operation, and personnel comfort. | Coordinate dehumidification with cooling and reheat so moisture is removed without creating excessive temperature variation. |
| Air cleanliness | Particle classification | Cleanroom classes are selected according to the maximum permitted airborne particle concentration at specified particle sizes. | Dehumidifiers must not introduce particles, fibers, oil aerosols, or corrosion products into the clean air stream. | Use suitable prefilters and final filters, maintain positive pressure where required, and perform airborne-particle classification testing. |
| Filtration | Final air filtration | High-efficiency final filters are commonly used in cleanroom air-handling systems; the exact efficiency depends on the room classification and risk assessment. | Filtration removes particles generated by equipment, ductwork, maintenance activity, and incoming air. | Conduct filter integrity testing, pressure-drop monitoring, airflow testing, and documented filter-change control. |
| Airflow | Air-change rate | Non-unidirectional cleanrooms may use approximately 10–60 air changes per hour, depending on classification, occupancy, process, and room layout. | Higher airflow can dilute and remove airborne contamination, but it also increases sensible and latent cooling loads. | Calculate airflow from cleanliness, heat load, moisture load, pressure cascade, and recovery requirements instead of selecting a rate solely by rule of thumb. |
| Airflow | Unidirectional airflow | Typical design velocities are often approximately 0.36–0.54 m/s for vertical or horizontal unidirectional airflow applications. | A consistent, low-turbulence airflow pattern helps sweep particles away from critical work zones. | Verify velocity uniformity, airflow visualization, filter coverage, and recovery after disturbance. |
| Pressure control | Pressure cascade | Adjacent rooms are commonly maintained with a pressure differential of approximately 5–15 Pa, subject to facility design and risk assessment. | Positive pressure helps prevent infiltration from less-clean areas. Negative pressure may be required for containment applications. | Monitor room-to-room pressure continuously or at defined intervals and verify door operation and leakage paths. |
| Moisture load | Main sources of moisture | Typical sources include outdoor ventilation air, infiltration, people, wet processes, cleaning, open liquids, and equipment exhaust. | The total latent load determines the required dehumidifier capacity and operating stability. | Perform a moisture-load calculation for summer design conditions, peak occupancy, cleaning periods, and abnormal operating scenarios. |
| Capacity selection | Moisture-removal capacity | Capacity should be stated as kg/h or kg/day at a defined entering-air temperature, humidity, airflow, and outlet dew point. | A nominal capacity without test conditions cannot be reliably compared between systems. | Require certified or documented performance data at the actual design conditions and include an appropriate safety margin. |
| Heat management | Reheat and sensible heat | Dehumidification can add heat to the air, especially when compressors, regeneration heaters, or desiccant wheels are operating. | Without coordinated cooling or reheat, the room may exceed its temperature limit even when humidity is controlled. | Balance cooling, dehumidification, regeneration, heat recovery, and reheat using a complete psychrometric analysis. |
| Materials and hygiene | Internal construction | Common requirements include smooth, cleanable, corrosion-resistant surfaces and sealed insulation located outside the airstream. | These features reduce particle generation, microbial harborage, corrosion, and contamination risk. | Inspect drain pans, coils, seals, access panels, fasteners, and internal finishes during commissioning and maintenance. |
| Condensate management | Drainage system | Condensate drains should have adequate slope, appropriate traps, accessible cleanouts, and no standing water in the air-handling section. | Poor drainage can cause microbial growth, re-entrainment of droplets, odors, corrosion, and contamination. | Test drainage under full load and inspect the pan, trap, piping, and drain termination at scheduled intervals. |
| Control strategy | Sensor placement | Humidity and temperature sensors may be installed in return air, supply air, representative room locations, and critical process zones. | Incorrect placement can cause delayed response, false readings, or unstable control. | Locate sensors away from supply-air jets, doors, heat sources, and direct contact with wet surfaces. Calibrate them periodically. |
| Energy performance | Energy considerations | Major energy consumers include fans, compressors, regeneration heaters, cooling equipment, and reheat systems. | Continuous high-airflow and low-dew-point operation can create a significant electrical and thermal load. | Use variable-speed drives, heat recovery, demand-based control, optimized setpoints, and operating schedules where the process permits. |
| Applications | Pharmaceutical and medical-product areas | Humidity is selected according to product sensitivity, formulation, packaging, sterility strategy, and process validation. | Moisture control can support powder handling, prevent material degradation, and improve process consistency. | Define environmental limits in validated procedures and document alarms, excursions, corrective actions, and recovery time. |
| Applications | Electronics and precision manufacturing | Many facilities use controlled humidity to reduce electrostatic-discharge risk and limit corrosion; the exact range depends on the product and ESD program. | Very dry air can increase static risk, while excessive humidity can promote corrosion and affect sensitive materials. | Coordinate humidity control with grounding, ionization, conductive flooring, packaging, and ESD monitoring. |
| Applications | Battery and moisture-sensitive material processing | Dry-room environments may require dew points well below 0°C, with the target determined by the chemistry and process stage. | Low moisture reduces unwanted reactions and helps protect moisture-sensitive materials during processing and storage. | Use low-leakage enclosures, dedicated airlocks, continuous dew-point monitoring, and verified personnel/material transfer procedures. |
| Commissioning | Performance qualification | Testing commonly includes temperature, humidity or dew point, airflow, pressure differential, particle concentration, filter integrity, and recovery time. | Commissioning confirms that the installed system meets the design intent under normal and defined worst-case conditions. | Use approved test protocols, calibrated instruments, acceptance criteria, recorded data, and documented deviations. |
| Maintenance | Routine service requirements | Typical tasks include filter inspection, coil cleaning, drain inspection, sensor calibration, desiccant inspection, belt checks, and alarm testing. | Maintenance preserves moisture-removal capacity, air cleanliness, energy efficiency, and control accuracy. | Set maintenance intervals according to operating hours, environmental exposure, contamination risk, and manufacturer-independent facility procedures. |
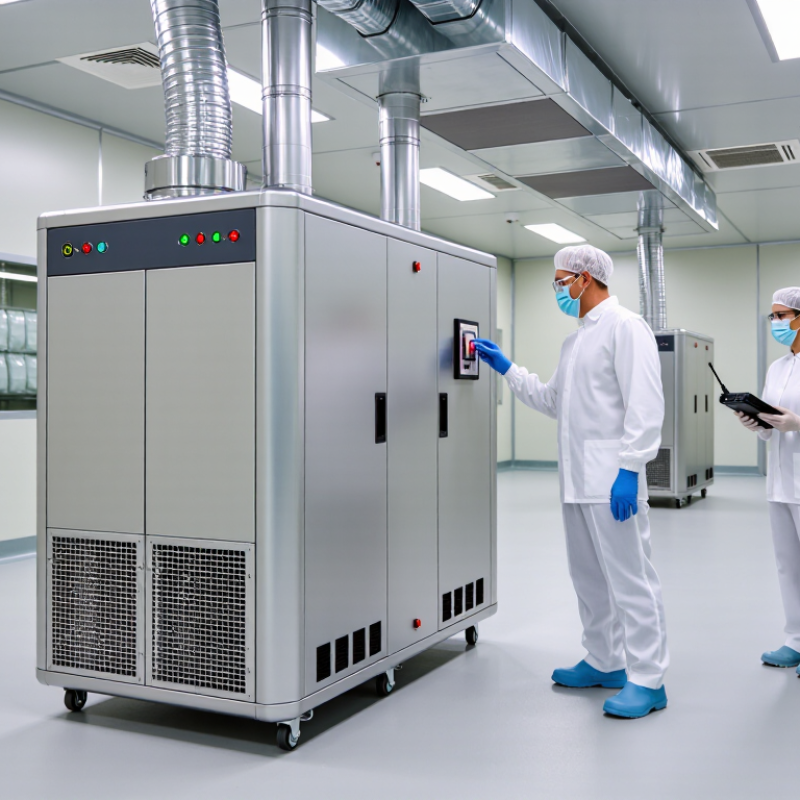
A cleanroom dehumidifier controls moisture that ordinary air-conditioning may not remove reliably. It draws humid air across a cooling coil or desiccant material. The system then returns drier air to the controlled space. Desiccant units often perform better at low humidity levels. Refrigerant-based units can suit moderate moisture loads. Selection depends on temperature, airflow, room pressure, and production requirements.
Maintenance protects both cleanliness and performance. Inspect filters, coils, seals, drain lines, and desiccant surfaces on a documented schedule. A blocked filter can reduce airflow and increase energy use. A damaged door seal may quietly raise humidity for hours. Technicians should compare sensor readings with calibrated references. Monitor relative humidity, dew point, temperature, pressure, and alarm history. Trend data often reveals gradual drift before a serious deviation occurs. Still, alarms are not enough. People must investigate the cause.
Tips: Keep sensors away from supply-air turbulence. Record readings at fixed times. Check drains after heavy operation. Clean carefully, not aggressively. Choose a unit with suitable capacity, accessible components, corrosion-resistant materials, and clear maintenance access. Allow spare capacity for door openings and seasonal moisture changes. Oversizing can cause unstable cycling, while undersizing creates continuous strain. Perfect control is rarely realistic. Recheck assumptions after the room begins operating.
We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Do you consent to the use of ALL cookies?
901 2nd Court West
Birmingham, AL 35204
Sales: 866.481.4036
Logistics/Ops: 866.481.4036
2101 Dralle Road
University Park, IL 60466
Sales: 708.813.9070
Logistics/Ops: 708.235.4200
400 E. 13th Street
Little Rock, AR 72114
Sales: 866.760.5344
Logistics/Ops: 866.760.5344
225 Collins Road
Elkhart, IN 46515
Sales: 574.295.0214
Logistics/Ops: 574.607.4611
601 Berryman Pike
Tipton, IN 46072
Sales: 800.897.7591
Logistics/Ops: 800.897.7591
3900 Uvalda Street
Denver, CO 80239
Sales: 303.706.8000
Ops/Logistics: 303.576.8398
510 3rd Street E
Milan, IL 61264
Sales: 800.322.1052
Logistics/Ops: 800.322.1052
1660 E. Aurora
Des Moines, IA 50313
Sales: 800.671.1660
Logistics: 800.671.1660
86554 Gene Lasserre Blvd.
Yulee, FL 32097
Sales: 904.253.3060
Logistics/Ops: 904.225.3000
694 S.E. County Road 245
Lake City, FL 32025
Sales: 800.727.6706
Logistics/Ops: 386.752.7412
210 Neptune Road
Auburndale, FL 33823
Sales: 863.967.1131
Logistics/Ops: 863.777.9814
4601 McCoy Drive
Pensacola, FL 32503
Sales: 850.308.7030
Logistics/Ops: 850.434.5502
815 South 56th Street
Tampa, FL 33619
Sales: 813.302.1940
Logistics/Ops: 813.621.1352
200 Hosea Road
Lawrenceville, GA 30046
Sales: 770.953.7575
Logistics/Ops: 770.513.6000
Branch Product Guide
Branch Line Card
Moulding Offering
Cedar Offering
Column Offering
8173 Hwy. 165 North
Monroe, LA 71211
Sales: 800.256.4165
Logistics/Ops: 800.256.4165
508 Warren Avenue
Portland, ME 04103
Sales: 207.888.2331
Logistics/Ops: 207.797.6565
4300 Georgia Pacific Blvd.
Frederick, MD 21704
Sales: 301.798.7474
Logistics/Ops: 301.874.8000
419 Maple Street
Bellingham, MA 02019
Sales: 508.449.0535
Logistics/Ops: 508.966.5500
825 Buchanan Ave SW
Grand Rapids, MI 49507
Sales: 877.800.1180
Logistics/Ops: 616.278.0909
995 Pacific St. NW
Aitkin, MN 56431
Sales: 800.432.3727
Logistics/Ops: 218.212.7770
1102 Port Terminal Drive
Duluth, MN 55802
Sales: 800.951.9899
Logistics/Ops: 800.851.9899
9110 83rd Ave. North
Brooklyn Park, MN 55445
Sales: 763.425.0204
Logistics/Ops: 763.425.0204
910 E. Railroad Street
Long Beach, MS 39560
Sales: 866.535.4135
Logistics/Ops: 228.205.2400
1727 Warren Street
North Kansas City, MO 64116
Sales: 800.621.2611
Logistics/Ops: 800.621.2611
2123 North Golden
Springfield, MO 65803
Sales: 800.375.7891
Logistics/Ops: 800.375.7891
13860 Corp. Woods Trail
Bridgeton, MO 63044
Sales: 314.209.0800
Logistics/Ops: 314.209.0800
1109 South 19th Street
Omaha, NE 68108
Sales: 800.489.6637
Logistics/Ops: 800.489.6637
1 Luger Road
Denville, NJ 07834
Sales: 973-339-3539
Logistics/Ops: 973.625.1461
3720 Jeffrey Blvd.
Blasdell, NY 14219
Sales: 716.235.5989
Logistics/Ops: 716.825.6557
319 Yaphank Ave.
Yaphank, NY 11980
Sales: 631.358.5714
Logistics/Ops: 631.924.7401
3300 Parkside Drive
Charlotte, NC 28208
Sales: 800.839.2588
Logistics/Ops: 704.394.3172
1712 East D Street
Butner, NC 27509
Sales: 984.389.8200
Logistics/Ops: 919.575.3700
128 Foothills Drive
Statesville, NC 28687
Sales: 800.222.1414
Logistics/Ops: 704.394.3172
550 Munroe Falls Rd.
Tallmadge, OH 44278
Sales: 330.357.4506
Logistics/Ops: 330.794.1141
10347 Toebben Dr.
Independence, KY 41051
Sales: 859.298.3926
Logistics/Ops: 859.746.2250
450 N. MacArthur
Oklahoma City, OK 73127
Sales: 800.375.6025
Logistics/Ops: 800.375.6025
1680 North Aspen
Broken Arrow, OK 74012
Sales: 918.272.2212
Logistics/Ops: 918.272.2212
522 Bridge Street
Hunker, PA 15639
Sales: 878.217.2001
Logistics/Ops: 724.925.7285
4290 Atlanta Street
Charleston, SC 29418
Sales: 843.371.1420
Logistics/Ops: 843.554.8192
1040 S. Industrial Dr.
Erwin, TN 37650
Sales: 423.641.1005
Logistics/Ops: 423.742.5911
4287 Pilot Drive
Memphis, TN 38118
Sales: 901.365.2101
Logistics/Ops: 901.365.2101
700 Myatt Drive
Madison, TN 37115
Sales: 615.327.9547
Logistics/Ops: 629.777.4949
4747 Mark IV Parkway
Fort Worth, TX 76106
Sales: 866.323.5117
Logistics/Ops: 817.625.9091
6990 Market Avenue
El Paso, TX 79915
Sales: 915.778.6356
Logistics/Ops: 915.265.7200
2502 Wilson Road
Harlingen, TX 78552
Sales: 800.580.6711
Logistics/Ops: 800.580.6711
10,000 North Loop East
Houston, TX 77029
Sales: 713.921.1977
Logistics/Ops: 713.675.3544
702 East 44th St.
Lubbock, TX 79404
Sales: 866.454.6010
Logistics/Ops: 866.454.6010
535 N. WW White Road
San Antonio, TX 78219
Sales: 800.284.0488
Logistics/Ops: 210.333.8112
142 Pine Haven Shores Rd.
Shelburne, VT 05482
Sales: 802.800.2540
Logistics/Ops: 802.985.2512
4700 Bethlehem Road,
Richmond, VA 23230
Sales: 804.201.2400
Logistics/Ops: 804.342.1161
4516 N Barker Road
Spokane Valley, WA 99027
Phone: 509.892.9420
Toll free: 800.728.6157
8365 N. 76th Street
Milwaukee, WI 53223
Sales: 800.356.9245
Logistics/Ops: 800.356.9245
312 S. Chester Street
Sparta, WI 54656
Sales: 800.362.5864
Logistics/Ops: 800.362.5864
899 Grossman Drive
Schofield, WI 54476
Sales: 800.472.0017
Logistics/Ops: 800.472.0017