We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Buying Welded Steel Pipe is not simply a matter of choosing a diameter and requesting a low price. The pipe must match its service conditions, including pressure, temperature, fluid type, installation method, and expected lifespan. A pipe that looks perfect on a warehouse rack may fail when corrosion, vibration, or repeated loading enters the picture. Details decide performance.
James F. Lincoln, a respected welding-industry pioneer, said, “The quality of the weld is only as good as the quality of the welder.” That principle remains useful when evaluating welded pipe. Buyers should examine the manufacturing process, welding method, seam quality, dimensional tolerances, material grade, and inspection records. Mill certificates matter. So do traceability markings, hydrostatic testing, and suitable nondestructive examination. However, paperwork alone cannot replace technical judgment. A certificate may be complete, yet the product may still be unsuitable for a specific environment.
This guide presents ten practical tips for buying Welded Steel Pipe with greater confidence. It considers wall thickness, outside diameter, steel chemistry, weld integrity, surface condition, coating requirements, and supplier capability. It also explains why recognized standards should be checked against the project specification, not accepted blindly. Standards differ by application and market. A cheaper quotation can become expensive after delays, rejected batches, or premature repairs. That sounds simple. It is not always simple. Even experienced buyers can overlook storage conditions, pipe-end protection, or compatibility with existing fittings. Careful questions, clear documentation, and independent verification create a more reliable purchasing decision.
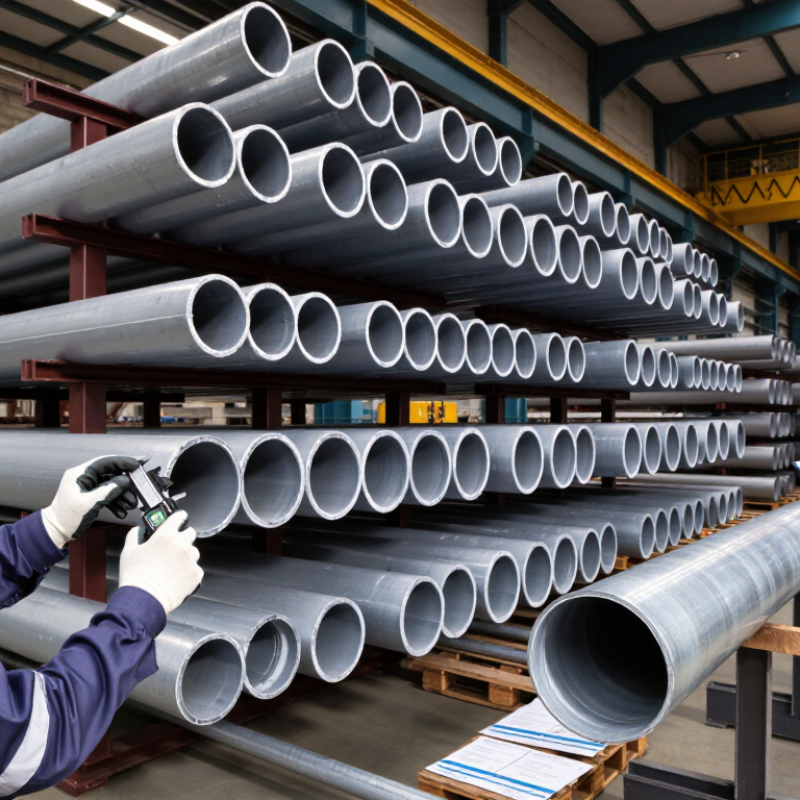
When buying welded steel pipe, define its application before comparing prices. Identify what the pipe will carry, such as water, steam, air, or process fluid. Record operating pressure, temperature, flow rate, and expected service life. A pipe for chilled water may fail in a hot, corrosive line. Small differences matter.
Check the required outside diameter, schedule, seam type, and connection method. Consider whether the pipe will be buried, exposed outdoors, or installed inside a plant. Moisture, soil chemicals, vibration, and repeated heating can change performance. Ask for mill test reports, dimensional records, and inspection results. Confirm that documents match the delivered heat number. A clean surface is not proof of reliable welding. I once overlooked installation vibration in an early specification, and the design needed revision. That mistake was avoidable.
Use recognized industry standards, but do not treat a standard as a complete design. Requirements differ between structural service, low-pressure water, and critical process systems. Discuss testing, including hydrostatic or nondestructive examination, before placing the order. Clarify tolerances, coating needs, end protection, and storage conditions. Even correct pipe can deteriorate when left uncovered in standing water. Recheck the application with the installer. Their field experience may reveal access, alignment, or drainage problems that drawings miss.
Tip 1: Match the steel grade to the working environment, not just the purchase price. Carbon steel suits many water and structural applications, while low-alloy grades may perform better under pressure or colder conditions. Check temperature, fluid chemistry, pressure, and required strength before choosing. A stronger grade is not automatically safer.
Tip 2: Select the manufacturing method according to pipe size, wall thickness, and service demands. Electric resistance welded pipe often provides consistent dimensions for general applications. Spiral welded pipe can offer practical cost advantages for large diameters. Longitudinal submerged arc welding may suit heavy-wall pipe and demanding infrastructure. The weld matters greatly.
Ask for material test certificates, heat numbers, dimensional reports, and inspection records. These documents support traceability from steel plate to finished pipe. Confirm weld inspection methods, such as ultrasonic or radiographic testing, when the application requires higher confidence. Hydrostatic testing may also be necessary.
Tip 3: Inspect the pipe before installation. Look for dents, uneven ends, coating damage, and visible weld irregularities. Measure outside diameter and wall thickness at several points. Small variations can complicate fitting later. I have seen specifications appear correct while poor storage caused avoidable corrosion. Protect pipe from standing water and direct soil contact. Check twice.
Before ordering welded steel pipe, treat the stated dimensions as measurements, not marketing promises. Ask for the outside diameter, length tolerance, and measuring method used by the supplier. At receiving inspection, use a calibrated tape, micrometer, and straightedge on several random pipes. Measure near both ends and at the middle. Small differences can affect fit-up, bending, and installation time. I have seen a pipe pass a visual check, then fail during assembly because its diameter varied.
Wall thickness deserves equal attention. Do not rely on one reading, especially near the weld seam. Take measurements around the circumference and compare them with the purchase specification. Ultrasonic testing can reveal local thinning, but the equipment must be calibrated and operated by trained personnel. Ask for inspection records that identify heat numbers, test methods, and acceptance criteria. Paperwork is useful. It is not proof by itself. Match the records to the bundle markings before approval.
Surface quality often reveals how carefully the pipe was made and handled. Look for cracks, laminations, deep scratches, dents, rust scale, and uneven weld reinforcement. Light surface discoloration may be harmless, while a sharp groove can reduce service reliability. Run a clean cloth over suspicious areas and inspect them under strong, angled light. Do not automatically reject every cosmetic mark; judge its depth, location, and effect on coating or fit. Specifications can be unclear, and my own early inspections were sometimes too subjective. Record photographs, readings, and rejected pieces, then ask a qualified inspector to review uncertain findings.
| No. | Buying Tip | What to Verify | Practical Check and Reference Data | Required Evidence |
|---|---|---|---|---|
| 1 | Confirm the applicable standard | Specify the product standard, grade, manufacturing process, and intended service before placing an order. | Common specifications include ASTM A53 for black or galvanized welded and seamless steel pipe and ASTM A500 for structural tubing. The selected standard should match the application and project requirements. | Purchase specification, applicable standard, grade designation, and approved technical data sheet. |
| 2 | Check outside diameter | Measure the outside diameter at several positions along each sampled pipe, avoiding the weld bead and damaged ends. | For a nominal 2 in pipe, the standard outside diameter is commonly 2.375 in, or approximately 60.3 mm. Compare the measured value with the tolerance stated in the purchase standard. | Calibrated vernier caliper or outside micrometer readings recorded by pipe number or batch. |
| 3 | Verify wall thickness | Measure wall thickness at multiple points around the circumference and at both ends where practical. | A nominal 2 in Schedule 40 pipe has a listed wall thickness of 0.154 in, or approximately 3.91 mm. Nominal thickness is not the same as the minimum permitted thickness; always apply the ordered standard and tolerance. | Ultrasonic thickness report or micrometer readings, including instrument identification and calibration status. |
| 4 | Inspect length and end condition | Confirm random, fixed, or cut lengths, then inspect end squareness, burrs, bevels, threads, and coupling requirements. | Typical commercial pipe may be supplied in random lengths, often around 5.8–6.4 m, but the exact range must be stated in the order. Threaded ends should be clean and undamaged when threading is specified. | Length inspection record, end-finish description, and photographs of representative pipe ends. |
| 5 | Examine weld seam quality | Look for continuous fusion, excessive undercut, cracks, open seams, sharp projections, or visible lack of bonding. | The weld area should be uniform and free from defects that could impair service. Internal or external weld-bead removal should be confirmed when required by the specification or downstream fabrication process. | Visual inspection report and, when specified, nondestructive examination results such as ultrasonic or electromagnetic testing. |
| 6 | Assess surface quality | Check the outside and inside surfaces for deep pits, laminations, scale, corrosion, dents, gouges, and handling damage. | Minor superficial mill marks may be acceptable if they do not reduce the permitted wall thickness. Any repaired area should be evaluated against the governing standard rather than accepted by appearance alone. | Surface inspection checklist, defect photographs, repair records, and remaining-wall-thickness measurements where needed. |
| 7 | Verify straightness and roundness | Inspect the pipe for visible bowing, ovality, flattening, and local deformation that may interfere with installation. | Measure at least two perpendicular outside diameters at selected locations to identify ovality. Acceptance limits depend on the product standard, size, and application; do not use a general visual estimate as the final decision. | Straightness and diameter measurement log with sampling locations and acceptance criteria. |
| 8 | Review mechanical and chemical properties | Confirm yield strength, tensile strength, elongation, carbon content, and other elements required by the ordered grade. | For ASTM A53 Grade B pipe, typical specified minimum values include 240 MPa yield strength and 415 MPa tensile strength. Verify the exact edition and product type because requirements can vary by standard. | Material test certificate showing heat number, chemical analysis, tensile test results, and traceability to the supplied pipes. |
| 9 | Check coating or galvanizing condition | For coated or galvanized pipe, inspect coverage, adhesion, uniformity, bare spots, runs, blisters, and handling damage. | Galvanized surfaces should be continuous and reasonably uniform for the specified coating system. Coating thickness and repair requirements must be assessed according to the specified galvanizing or coating standard. | Coating or galvanizing certificate, thickness readings, visual inspection report, and repair procedure where applicable. |
| 10 | Confirm marking, packing, and traceability | Match pipe markings and bundle labels with the purchase order, heat number, grade, size, wall thickness, quantity, and inspection documents. | Each bundle should be protected against impact, contamination, and moisture accumulation during transport. Traceability should remain legible from receipt through installation. | Photographs of markings, packing list, heat-number traceability record, quantity check, and final release note. |
Inspection Note Dimensions, tolerances, testing frequency, and acceptance criteria must be finalized against the exact product standard and project specification stated in the purchase order.
10 Tips for Buying Welded Steel Pipe
Welding quality starts with a clear service specification. Define pressure, temperature, fluid, diameter, wall thickness, and corrosion exposure. Then match the pipe to recognized requirements, such as API Spec 5L, ASME B31.3, or ASTM material standards. ISO 3834 also helps assess welding quality systems. According to the ISO Survey 2023, more than one million ISO 9001 certificates were reported worldwide. Certification shows process control, but it does not guarantee every pipe.
Tip 1: Ask for the exact welding procedure specification, not a generic template. Tip 2: Check welder qualification records and procedure qualification tests. Tip 3: Request heat numbers, mill certificates, and traceability documents. Traceability should connect the pipe, weld, test result, and shipment record. Small gaps matter.
Testing should reflect the pipe’s actual service risk. Hydrostatic testing can reveal leakage under pressure. Ultrasonic testing can detect internal discontinuities without cutting the pipe. Radiographic testing may expose lack of fusion or trapped defects. Confirm acceptance criteria before production begins. The 2024 World Steel Association data recorded about 1.88 billion tonnes of crude steel production globally, making supply-chain consistency a serious concern. Tip 4: Verify test methods and sampling rates. Tip 5: Review nonconformance reports. Tip 6: Inspect surface condition, weld reinforcement, ovality, and end preparation. A certificate can look reassuring. It may still cover a factory system, not your exact heat. An independent inspection is useful, though it adds time and cost.
The chart compares minimum yield and tensile strength requirements for selected welded-pipe grades commonly referenced in ASTM A53 and API 5L specifications. Strength values are shown in MPa; actual requirements may vary by product grade, pipe diameter, wall thickness, PSL level, and edition of the applicable standard.
Compare Suppliers, Pricing, Delivery, and After-Sales Support
Buying welded steel pipe requires more than comparing unit prices. I check the supplier’s production experience, quality records, and inspection process. Ask for material certificates, weld inspection reports, dimensional tolerances, and coating details. A reliable supplier should explain how samples are tested and stored.
Do not compare quotations line by line only. One price may include cutting, packing, testing, and transport, while another excludes them. Request a clear cost breakdown. I also compare payment terms, minimum order quantities, and replacement policies for damaged pipes. A cheaper offer can become expensive after delays or rework.
Delivery needs practical questions. Confirm production time, loading dates, packing methods, and shipping documents before placing an order. For large pipes, weak supports can cause dents during handling. I prefer suppliers who provide progress photos and tracking updates. It saves time.
After-sales support matters when site problems appear. Ask who handles claims, how quickly they respond, and what evidence they require. Keep inspection photos and receiving records. They can prevent arguments later.
I have sometimes focused too much on price. That was a mistake. A dependable supplier may cost slightly more but reduce project disruption. Still, service promises should be written clearly, not accepted as casual assurances.
We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Do you consent to the use of ALL cookies?
901 2nd Court West
Birmingham, AL 35204
Sales: 866.481.4036
Logistics/Ops: 866.481.4036
2101 Dralle Road
University Park, IL 60466
Sales: 708.813.9070
Logistics/Ops: 708.235.4200
400 E. 13th Street
Little Rock, AR 72114
Sales: 866.760.5344
Logistics/Ops: 866.760.5344
225 Collins Road
Elkhart, IN 46515
Sales: 574.295.0214
Logistics/Ops: 574.607.4611
601 Berryman Pike
Tipton, IN 46072
Sales: 800.897.7591
Logistics/Ops: 800.897.7591
3900 Uvalda Street
Denver, CO 80239
Sales: 303.706.8000
Ops/Logistics: 303.576.8398
510 3rd Street E
Milan, IL 61264
Sales: 800.322.1052
Logistics/Ops: 800.322.1052
1660 E. Aurora
Des Moines, IA 50313
Sales: 800.671.1660
Logistics: 800.671.1660
86554 Gene Lasserre Blvd.
Yulee, FL 32097
Sales: 904.253.3060
Logistics/Ops: 904.225.3000
694 S.E. County Road 245
Lake City, FL 32025
Sales: 800.727.6706
Logistics/Ops: 386.752.7412
210 Neptune Road
Auburndale, FL 33823
Sales: 863.967.1131
Logistics/Ops: 863.777.9814
4601 McCoy Drive
Pensacola, FL 32503
Sales: 850.308.7030
Logistics/Ops: 850.434.5502
815 South 56th Street
Tampa, FL 33619
Sales: 813.302.1940
Logistics/Ops: 813.621.1352
200 Hosea Road
Lawrenceville, GA 30046
Sales: 770.953.7575
Logistics/Ops: 770.513.6000
Branch Product Guide
Branch Line Card
Moulding Offering
Cedar Offering
Column Offering
8173 Hwy. 165 North
Monroe, LA 71211
Sales: 800.256.4165
Logistics/Ops: 800.256.4165
508 Warren Avenue
Portland, ME 04103
Sales: 207.888.2331
Logistics/Ops: 207.797.6565
4300 Georgia Pacific Blvd.
Frederick, MD 21704
Sales: 301.798.7474
Logistics/Ops: 301.874.8000
419 Maple Street
Bellingham, MA 02019
Sales: 508.449.0535
Logistics/Ops: 508.966.5500
825 Buchanan Ave SW
Grand Rapids, MI 49507
Sales: 877.800.1180
Logistics/Ops: 616.278.0909
995 Pacific St. NW
Aitkin, MN 56431
Sales: 800.432.3727
Logistics/Ops: 218.212.7770
1102 Port Terminal Drive
Duluth, MN 55802
Sales: 800.951.9899
Logistics/Ops: 800.851.9899
9110 83rd Ave. North
Brooklyn Park, MN 55445
Sales: 763.425.0204
Logistics/Ops: 763.425.0204
910 E. Railroad Street
Long Beach, MS 39560
Sales: 866.535.4135
Logistics/Ops: 228.205.2400
1727 Warren Street
North Kansas City, MO 64116
Sales: 800.621.2611
Logistics/Ops: 800.621.2611
2123 North Golden
Springfield, MO 65803
Sales: 800.375.7891
Logistics/Ops: 800.375.7891
13860 Corp. Woods Trail
Bridgeton, MO 63044
Sales: 314.209.0800
Logistics/Ops: 314.209.0800
1109 South 19th Street
Omaha, NE 68108
Sales: 800.489.6637
Logistics/Ops: 800.489.6637
1 Luger Road
Denville, NJ 07834
Sales: 973-339-3539
Logistics/Ops: 973.625.1461
3720 Jeffrey Blvd.
Blasdell, NY 14219
Sales: 716.235.5989
Logistics/Ops: 716.825.6557
319 Yaphank Ave.
Yaphank, NY 11980
Sales: 631.358.5714
Logistics/Ops: 631.924.7401
3300 Parkside Drive
Charlotte, NC 28208
Sales: 800.839.2588
Logistics/Ops: 704.394.3172
1712 East D Street
Butner, NC 27509
Sales: 984.389.8200
Logistics/Ops: 919.575.3700
128 Foothills Drive
Statesville, NC 28687
Sales: 800.222.1414
Logistics/Ops: 704.394.3172
550 Munroe Falls Rd.
Tallmadge, OH 44278
Sales: 330.357.4506
Logistics/Ops: 330.794.1141
10347 Toebben Dr.
Independence, KY 41051
Sales: 859.298.3926
Logistics/Ops: 859.746.2250
450 N. MacArthur
Oklahoma City, OK 73127
Sales: 800.375.6025
Logistics/Ops: 800.375.6025
1680 North Aspen
Broken Arrow, OK 74012
Sales: 918.272.2212
Logistics/Ops: 918.272.2212
522 Bridge Street
Hunker, PA 15639
Sales: 878.217.2001
Logistics/Ops: 724.925.7285
4290 Atlanta Street
Charleston, SC 29418
Sales: 843.371.1420
Logistics/Ops: 843.554.8192
1040 S. Industrial Dr.
Erwin, TN 37650
Sales: 423.641.1005
Logistics/Ops: 423.742.5911
4287 Pilot Drive
Memphis, TN 38118
Sales: 901.365.2101
Logistics/Ops: 901.365.2101
700 Myatt Drive
Madison, TN 37115
Sales: 615.327.9547
Logistics/Ops: 629.777.4949
4747 Mark IV Parkway
Fort Worth, TX 76106
Sales: 866.323.5117
Logistics/Ops: 817.625.9091
6990 Market Avenue
El Paso, TX 79915
Sales: 915.778.6356
Logistics/Ops: 915.265.7200
2502 Wilson Road
Harlingen, TX 78552
Sales: 800.580.6711
Logistics/Ops: 800.580.6711
10,000 North Loop East
Houston, TX 77029
Sales: 713.921.1977
Logistics/Ops: 713.675.3544
702 East 44th St.
Lubbock, TX 79404
Sales: 866.454.6010
Logistics/Ops: 866.454.6010
535 N. WW White Road
San Antonio, TX 78219
Sales: 800.284.0488
Logistics/Ops: 210.333.8112
142 Pine Haven Shores Rd.
Shelburne, VT 05482
Sales: 802.800.2540
Logistics/Ops: 802.985.2512
4700 Bethlehem Road,
Richmond, VA 23230
Sales: 804.201.2400
Logistics/Ops: 804.342.1161
4516 N Barker Road
Spokane Valley, WA 99027
Phone: 509.892.9420
Toll free: 800.728.6157
8365 N. 76th Street
Milwaukee, WI 53223
Sales: 800.356.9245
Logistics/Ops: 800.356.9245
312 S. Chester Street
Sparta, WI 54656
Sales: 800.362.5864
Logistics/Ops: 800.362.5864
899 Grossman Drive
Schofield, WI 54476
Sales: 800.472.0017
Logistics/Ops: 800.472.0017
