We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Why Choose High Carbon Steel Coil for Global Sourcing?
High Carbon Steel Coil remains a practical choice for springs, saw blades, knives, wires, and wear-resistant components. Its elevated carbon content supports higher hardness and tensile strength after suitable heat treatment. However, “high carbon” is not a universal grade. Carbon limits, alloy additions, and delivery conditions vary across ASTM, EN, JIS, and other standards.
The scale of global steel production supports broad sourcing options. The World Steel Association’s World Steel in Figures 2024 reported approximately 1.892 billion tonnes of crude steel production in 2023. This extensive production base can improve supplier availability, but volume alone does not guarantee quality. The OECD’s Steel Outlook 2023 also highlighted persistent capacity pressures and uneven market conditions. Buyers should therefore examine mill capability, not only quoted prices.
Small details matter.
A sourcing team should verify chemistry, coil weight, thickness tolerance, flatness, surface condition, and edge quality. Mill test certificates should match the actual heat number, with traceable inspection records. In practical purchasing, a bright, clean coil may still fail during stamping if hardness varies across its width. Conversely, a lower-priced coil can create higher costs through slitting waste, delayed customs clearance, or inconsistent heat treatment.
The International Trade Centre and UN Comtrade provide useful trade statistics, but high carbon products may fall under different tariff classifications. This makes direct comparison imperfect. The best decision combines laboratory evidence, supplier audits, sample trials, and realistic logistics planning. High Carbon Steel Coil is not automatically the best option. Its value depends on verified performance, stable supply, and the buyer’s actual processing conditions.
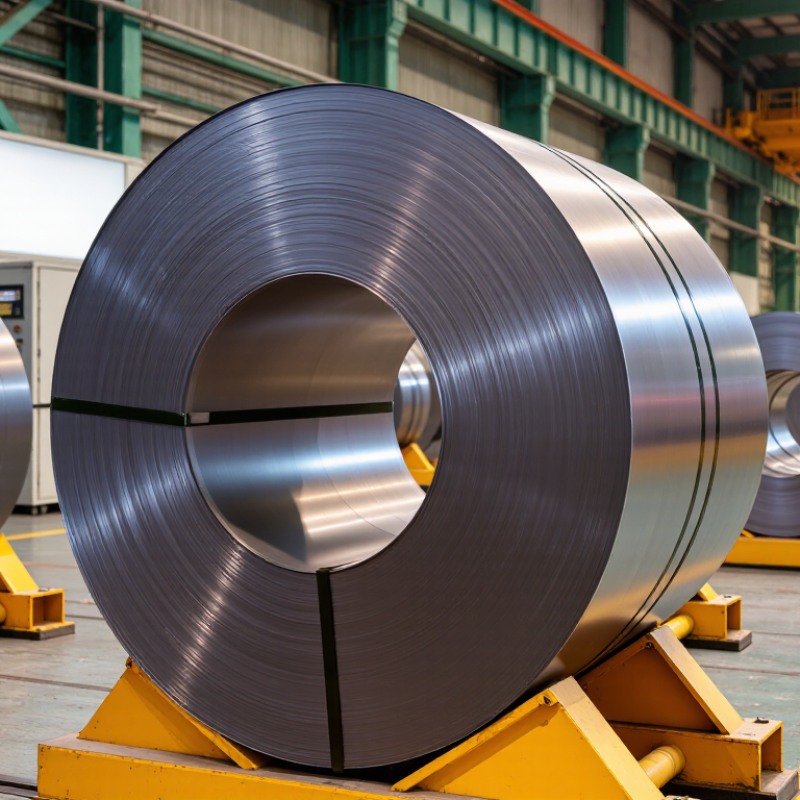
High carbon steel coil is flat-rolled steel wound into compact rolls for transport and processing. In common industry practice, it contains about 0.60% to 1.00% carbon by weight. Exact limits vary by standard and application. Higher carbon content improves hardness, tensile strength, and wear resistance after heat treatment. It can support spring components, cutting edges, rails, and abrasion-resistant parts. It is not simply stronger steel. It is also less forgiving during forming and welding.
The World Steel Association’s World Steel in Figures 2024 reports approximately 1.9 billion tonnes of crude steel production in 2023. However, that report does not separate high carbon coil volumes. This limitation matters when evaluating supply claims. Buyers should request heat-level chemical analysis, thickness tolerance, surface condition, and mechanical test results. Carbon content alone cannot confirm coil quality. Manganese, sulfur, phosphorus, cooling practice, and annealing history also affect performance. A coil may look uniform.
The International Energy Agency links iron and steel production with roughly 7% to 9% of global energy-related carbon dioxide emissions. Responsible sourcing therefore includes carbon data, recycled content, and traceable production records. An environmental product declaration can improve comparison, though reporting quality still varies between suppliers. One practical mistake is treating hardness as proof of reliability. Excessive hardness may create cracking during slitting or forming. Global buyers should match the grade with the final process, not just the purchase price. Their specification may still be incomplete.
High carbon steel coil begins with carefully controlled raw materials, usually iron-bearing feedstock, scrap, and carbon-adjusting alloys. In a basic oxygen furnace or electric arc furnace, operators melt the charge and test its chemistry. Carbon content commonly ranges from about 0.60% to 1.00%, depending on the required grade and application. Secondary metallurgy removes unwanted gases and adjusts manganese, silicon, and sulfur levels. Small chemistry changes matter.
The molten steel then enters continuous casting, where water-cooled molds form slabs. Reheating softens each slab before hot rolling reduces it through multiple stands. The strip becomes thinner, longer, and visibly brighter under pressure. Controlled cooling influences hardness and pearlite formation. Coiling temperature must remain consistent. Otherwise, the coil may show uneven mechanical properties across its width. Pickling can remove scale, while cold rolling may improve thickness accuracy and surface quality. Annealing or spheroidizing is sometimes added for demanding forming or wire applications.
The World Steel Association reported 1,888.2 million tonnes of crude steel production in 2023. That scale explains why process consistency matters in global sourcing. The International Energy Agency estimates steelmaking creates roughly 7% to 9% of global energy-related carbon dioxide emissions. Buyers should therefore review mill test certificates, heat numbers, dimensional tolerances, and surface inspection records. A low price alone proves little. In practice, even well-managed production is not flawless; handling marks, coil-edge damage, or slight hardness variation can still appear.
High carbon steel coil is valued for its strength, hardness, and resistance to repeated wear. These properties make it suitable for springs, blades, cutting parts, and industrial components exposed to friction. Its carbon content supports strong performance after heat treatment. The final hardness depends on chemistry, thickness, cooling, and processing control.
In practical sourcing, consistent coil thickness matters. Small variations can affect stamping pressure, cutting accuracy, and finished-part balance. A reliable supplier should provide mill test certificates, dimensional records, surface inspection results, and traceable heat numbers. High carbon steel is not the easiest material to form. It may show greater springback and lower weldability than mild steel. That limitation deserves attention before production begins. I have seen designs fail when engineers considered strength but ignored forming conditions.
Tips: Confirm the required carbon range, hardness, coil width, and thickness tolerance before ordering. Request sample data and review heat-treatment requirements. Check the surface for scale, scratches, edge cracks, and uneven coiling. Test a small batch under real forming conditions. Laboratory figures can look excellent, yet shop-floor behavior may differ. Include packaging details for long-distance transport, especially moisture protection and edge safety. Good documentation reduces uncertainty, but it cannot replace physical inspection.
Key properties of high carbon steel coil are closely related to its carbon content. The representative chemistry ranges below show how carbon increases across common SAE/AISI high-carbon steel grades, supporting higher hardness, wear resistance, and strength after suitable heat treatment.
Carbon content is shown as weight percent. Higher-carbon grades generally offer improved hardness and wear resistance, while requiring greater attention to forming, welding, and heat-treatment control.
High carbon steel coil supports demanding applications where hardness, strength, and wear resistance matter. Manufacturers use it for springs, saw blades, agricultural tools, rail components, and stamped wear parts. Global sourcing can widen supplier options and improve access to specific carbon ranges, thicknesses, and surface finishes. It may also reduce purchasing costs when production volumes are stable.
Experienced buyers compare more than the quoted price. They review chemical composition, tensile strength, hardness, coil weight, edge condition, and dimensional tolerances. Mill test certificates provide useful evidence, but independent testing can reveal inconsistencies. Packaging also matters. A tightly secured coil with moisture protection arrives more safely after long sea transport. A low price can mislead. Freight, inspection, storage, and possible rework may change the final cost.
Tips: Confirm the required grade before requesting offers. Ask for sample data and recent inspection records. Check whether the supplier can maintain consistent thickness across the coil. Plan delivery buffers for port delays and production scheduling. Some buyers overlook unloading equipment, which can create avoidable handling risks. No sourcing plan is flawless; review supplier performance after each shipment. High carbon steel also needs suitable forming and heat-treatment controls, because excessive hardness can complicate fabrication and increase cracking risk.
High carbon steel coil suits springs, blades, saw components, and wear-resistant parts. Its value depends on controlled chemistry, not carbon content alone. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023. Such scale creates options, but also inconsistent supplier quality.
Start with the intended application. For cold-rolled high-carbon strip, ASTM A684/A684M may define grades, testing, and dimensional requirements. Other products may require different standards. Ask for a mill test certificate showing carbon, manganese, sulfur, phosphorus, hardness, tensile strength, and elongation. Coil width, thickness tolerance, edge condition, surface defects, and inner diameter also need written limits. Small deviations can cause cracking during stamping.
Traceability matters. Each coil should carry a heat number linked to production records, inspection results, and packing details. ISO 9001 certification supports process control, but it does not replace product testing. Request recent third-party inspection records and verify laboratory competence under ISO/IEC 17025 where appropriate. Audit storage conditions too. Moisture, poor wrapping, and uneven stacking can damage otherwise compliant steel. No checklist is flawless. A supplier may provide perfect documents and still miss a recurring surface defect. Trial orders, retained samples, and independent verification offer stronger evidence than price alone.
| Category | Data Dimension | Typical Reference Data | Quality or Sourcing Significance | Recommended Verification |
|---|---|---|---|---|
| Material Characteristics | ||||
| Material | Carbon steel type | High carbon steel, generally containing approximately 0.60% to 1.00% carbon by mass, depending on the specified grade. | Higher carbon content provides increased hardness, strength, and wear resistance after suitable heat treatment. | Review the chemical composition report and confirm the applicable grade standard. |
| Common grades | Representative grades | SAE/AISI 1060: about 0.55%–0.65% C; SAE/AISI 1070: about 0.65%–0.75% C; SAE/AISI 1095: about 0.90%–1.03% C. Equivalent grades may differ by standard. | Grade selection should match the required hardness, forming capability, fatigue performance, and heat-treatment process. | Compare the mill certificate with the precise chemical limits in the purchase specification. |
| Typical applications | End-use suitability | Springs, saw blades, knives, scrapers, wear-resistant parts, agricultural components, and industrial cutting products. | High carbon steel is suitable where strength and wear resistance are more important than deep drawability or high weldability. | Request application references by product type, without relying only on a generic grade name. |
| Weldability | Process sensitivity | Generally limited compared with low-carbon steel because higher carbon content increases hardening and cracking risk in the heat-affected zone. | Welding may require qualified procedures, preheating, controlled cooling, and post-weld treatment. | Confirm welding restrictions and obtain a qualified welding procedure when welding is part of the application. |
| Mechanical and Dimensional Data | ||||
| Mechanical properties | Tensile strength | Condition-dependent. Cold-rolled or hardened high-carbon strip commonly ranges from approximately 700 MPa to above 2,000 MPa. | Strength varies significantly with grade, reduction, annealing, quenching, tempering, and delivery condition. | Specify the delivery condition and test method; verify results against ISO 6892-1 or ASTM A370 where applicable. |
| Mechanical properties | Yield strength | Condition-dependent; annealed material may be substantially lower than cold-worked or hardened material. Use the contractual grade limit rather than a generic range. | Yield strength affects forming, spring-back, and load-bearing performance. | Require yield strength values on the inspection certificate when relevant to the design. |
| Mechanical properties | Elongation | Often approximately 2%–25%, depending on carbon level, thickness, cold reduction, and heat-treatment condition. | Lower elongation generally indicates reduced forming capability but may accompany higher strength and hardness. | Define the gauge length and test standard because reported elongation values are not directly comparable otherwise. |
| Hardness | Hardness range | Annealed material may be around 180–250 HBW; hardened and tempered products can commonly range from about 40 to 62 HRC, depending on grade and treatment. | Hardness is a key indicator for springs, blades, cutting edges, and wear parts. | Specify the hardness scale, test location, sampling frequency, and acceptance range. |
| Dimensions | Typical thickness capability | Approximately 0.15–6.00 mm for many cold-rolled coil supply programs; actual capability depends on the mill and product form. | Thickness capability influences material utilization, forming performance, and production yield. | Request a dimensional capability chart and confirm minimum order quantities for non-standard thicknesses. |
| Dimensions | Typical width capability | Approximately 20–1,500 mm for coil products, subject to equipment, edge condition, and thickness limitations. | Width availability affects slitting plans, scrap rate, container loading, and downstream productivity. | Confirm maximum coil width, slit-width tolerance, edge condition, and coil weight limits. |
| Dimensional tolerance | Thickness and width tolerance | Must be defined by the selected product standard or purchase specification; tolerances are not universal across grades and sizes. | Unspecified tolerances can create fit, forming, and yield problems during production. | Use the applicable dimensional standard and include target, tolerance, measurement method, and sampling plan in the purchase order. |
| Quality Standards and Surface Requirements | ||||
| Product standard | High-carbon steel strip specification | ASTM A684/A684M is commonly used for high-carbon steel strip. EN 10132-4 covers cold-rolled narrow steel strip for quenching and tempering. | A recognized standard establishes requirements for chemistry, mechanical properties, dimensions, surface quality, and testing. | State the exact edition and grade designation in the request for quotation and purchase order. |
| Testing standard | Tensile testing | ISO 6892-1 or ASTM A370 may be used, provided the selected standard and test conditions are agreed in advance. | Consistent testing is essential for comparing suppliers and validating certificate data. | Check specimen direction, gauge length, test temperature, and laboratory identification. |
| Surface quality | Surface condition | Common requirements include a clean surface free from harmful cracks, seams, laps, rust scale, excessive pits, and damaging scratches. | Surface defects can reduce fatigue life, impair coating or plating, and cause rejection during slitting or stamping. | Define inspection lighting, defect limits, coil sampling length, and acceptable surface finish. |
| Edge quality | Mill edge or slit edge | Available as mill edge or slit edge, depending on the intended processing route and dimensional requirements. | Edge burrs, cracks, or camber may affect feeding, blanking, spring forming, and operator safety. | Specify edge type, maximum burr height, camber limit, and edge-crack acceptance criteria. |
| Flatness | Flatness and shape | Requirements should cover coil set, crossbow, waviness, and camber; numerical limits depend on the applicable standard and thickness. | Poor shape control can cause feeding errors, dimensional variation, and increased scrap in automated lines. | Request flatness measurements using an agreed method and sampling location. |
| Corrosion protection | Packaging and rust prevention | Common measures include dry wrapping, waterproof outer packaging, corrosion-inhibiting paper or film, and secure eye or circumference protection. | Proper protection reduces transit damage and corrosion during ocean freight or extended storage. | Approve a packaging specification covering humidity exposure, coil orientation, lifting points, and storage conditions. |
| Global Supplier Selection Criteria | ||||
| Traceability | Heat and coil identification | Each coil should be traceable to a heat number, production date or batch, grade, dimensions, and inspection records. | Traceability supports claims handling, root-cause analysis, and controlled release into production. | Match coil tags, packing lists, mill certificates, and inspection reports before shipment. |
| Documentation | Inspection certificate | Certificate should normally include chemical analysis, mechanical test results, dimensions, delivery condition, standard, heat number, and coil weight. | Complete documentation reduces customs, receiving, and quality-assurance risks. | Require certificates before shipment or before final payment, as agreed contractually. |
| Quality system | Manufacturing controls | Prefer documented control of melting, rolling, annealing, heat treatment, slitting, calibration, nonconformance handling, and final inspection. | Process control is more reliable than evaluating quality only from a final sample. | Review current quality certificates, process flow, inspection plans, and corrective-action records. |
| Sampling | Pre-shipment inspection | Typical checks include chemistry review, thickness and width measurements, surface inspection, hardness or tensile testing, coil weight, and packaging condition. | Independent or buyer-appointed inspection can reduce the risk of receiving nonconforming material. | Define the sampling level, acceptance criteria, test laboratory, and inspection hold point. |
| Commercial fit | Minimum order and lead time | Minimum order quantities and lead times vary by grade, thickness, width, heat-treatment condition, and slitting requirements. | Commercial flexibility is important when validating a new grade or managing variable demand. | Request separate quotations for standard sizes, custom sizes, trial coils, and repeat-order quantities. |
| Logistics | Coil weight and loading | Coil weights should be matched to the buyer’s decoiler, crane, storage rack, container payload, and unloading equipment. | Incorrect coil weight can create handling hazards, equipment downtime, and additional transport cost. | Specify minimum and maximum coil weight, inner diameter, outer diameter, eye orientation, and securing method. |
| Payment risk | Commercial safeguards | Use staged documentation, clearly defined inspection rights, agreed nonconformance remedies, and shipment release conditions. | Contractual controls help protect quality, delivery, and payment interests in cross-border sourcing. | Include standards, tolerances, inspection procedures, claims periods, and remedy terms in the contract. |
| Note: The numerical ranges are indicative industry reference values. Final acceptance limits must be based on the selected grade, product standard, delivery condition, thickness, heat treatment, and mutually agreed purchase specification. | ||||
We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Do you consent to the use of ALL cookies?
901 2nd Court West
Birmingham, AL 35204
Sales: 866.481.4036
Logistics/Ops: 866.481.4036
2101 Dralle Road
University Park, IL 60466
Sales: 708.813.9070
Logistics/Ops: 708.235.4200
400 E. 13th Street
Little Rock, AR 72114
Sales: 866.760.5344
Logistics/Ops: 866.760.5344
225 Collins Road
Elkhart, IN 46515
Sales: 574.295.0214
Logistics/Ops: 574.607.4611
601 Berryman Pike
Tipton, IN 46072
Sales: 800.897.7591
Logistics/Ops: 800.897.7591
3900 Uvalda Street
Denver, CO 80239
Sales: 303.706.8000
Ops/Logistics: 303.576.8398
510 3rd Street E
Milan, IL 61264
Sales: 800.322.1052
Logistics/Ops: 800.322.1052
1660 E. Aurora
Des Moines, IA 50313
Sales: 800.671.1660
Logistics: 800.671.1660
86554 Gene Lasserre Blvd.
Yulee, FL 32097
Sales: 904.253.3060
Logistics/Ops: 904.225.3000
694 S.E. County Road 245
Lake City, FL 32025
Sales: 800.727.6706
Logistics/Ops: 386.752.7412
210 Neptune Road
Auburndale, FL 33823
Sales: 863.967.1131
Logistics/Ops: 863.777.9814
4601 McCoy Drive
Pensacola, FL 32503
Sales: 850.308.7030
Logistics/Ops: 850.434.5502
815 South 56th Street
Tampa, FL 33619
Sales: 813.302.1940
Logistics/Ops: 813.621.1352
200 Hosea Road
Lawrenceville, GA 30046
Sales: 770.953.7575
Logistics/Ops: 770.513.6000
Branch Product Guide
Branch Line Card
Moulding Offering
Cedar Offering
Column Offering
8173 Hwy. 165 North
Monroe, LA 71211
Sales: 800.256.4165
Logistics/Ops: 800.256.4165
508 Warren Avenue
Portland, ME 04103
Sales: 207.888.2331
Logistics/Ops: 207.797.6565
4300 Georgia Pacific Blvd.
Frederick, MD 21704
Sales: 301.798.7474
Logistics/Ops: 301.874.8000
419 Maple Street
Bellingham, MA 02019
Sales: 508.449.0535
Logistics/Ops: 508.966.5500
825 Buchanan Ave SW
Grand Rapids, MI 49507
Sales: 877.800.1180
Logistics/Ops: 616.278.0909
995 Pacific St. NW
Aitkin, MN 56431
Sales: 800.432.3727
Logistics/Ops: 218.212.7770
1102 Port Terminal Drive
Duluth, MN 55802
Sales: 800.951.9899
Logistics/Ops: 800.851.9899
9110 83rd Ave. North
Brooklyn Park, MN 55445
Sales: 763.425.0204
Logistics/Ops: 763.425.0204
910 E. Railroad Street
Long Beach, MS 39560
Sales: 866.535.4135
Logistics/Ops: 228.205.2400
1727 Warren Street
North Kansas City, MO 64116
Sales: 800.621.2611
Logistics/Ops: 800.621.2611
2123 North Golden
Springfield, MO 65803
Sales: 800.375.7891
Logistics/Ops: 800.375.7891
13860 Corp. Woods Trail
Bridgeton, MO 63044
Sales: 314.209.0800
Logistics/Ops: 314.209.0800
1109 South 19th Street
Omaha, NE 68108
Sales: 800.489.6637
Logistics/Ops: 800.489.6637
1 Luger Road
Denville, NJ 07834
Sales: 973-339-3539
Logistics/Ops: 973.625.1461
3720 Jeffrey Blvd.
Blasdell, NY 14219
Sales: 716.235.5989
Logistics/Ops: 716.825.6557
319 Yaphank Ave.
Yaphank, NY 11980
Sales: 631.358.5714
Logistics/Ops: 631.924.7401
3300 Parkside Drive
Charlotte, NC 28208
Sales: 800.839.2588
Logistics/Ops: 704.394.3172
1712 East D Street
Butner, NC 27509
Sales: 984.389.8200
Logistics/Ops: 919.575.3700
128 Foothills Drive
Statesville, NC 28687
Sales: 800.222.1414
Logistics/Ops: 704.394.3172
550 Munroe Falls Rd.
Tallmadge, OH 44278
Sales: 330.357.4506
Logistics/Ops: 330.794.1141
10347 Toebben Dr.
Independence, KY 41051
Sales: 859.298.3926
Logistics/Ops: 859.746.2250
450 N. MacArthur
Oklahoma City, OK 73127
Sales: 800.375.6025
Logistics/Ops: 800.375.6025
1680 North Aspen
Broken Arrow, OK 74012
Sales: 918.272.2212
Logistics/Ops: 918.272.2212
522 Bridge Street
Hunker, PA 15639
Sales: 878.217.2001
Logistics/Ops: 724.925.7285
4290 Atlanta Street
Charleston, SC 29418
Sales: 843.371.1420
Logistics/Ops: 843.554.8192
1040 S. Industrial Dr.
Erwin, TN 37650
Sales: 423.641.1005
Logistics/Ops: 423.742.5911
4287 Pilot Drive
Memphis, TN 38118
Sales: 901.365.2101
Logistics/Ops: 901.365.2101
700 Myatt Drive
Madison, TN 37115
Sales: 615.327.9547
Logistics/Ops: 629.777.4949
4747 Mark IV Parkway
Fort Worth, TX 76106
Sales: 866.323.5117
Logistics/Ops: 817.625.9091
6990 Market Avenue
El Paso, TX 79915
Sales: 915.778.6356
Logistics/Ops: 915.265.7200
2502 Wilson Road
Harlingen, TX 78552
Sales: 800.580.6711
Logistics/Ops: 800.580.6711
10,000 North Loop East
Houston, TX 77029
Sales: 713.921.1977
Logistics/Ops: 713.675.3544
702 East 44th St.
Lubbock, TX 79404
Sales: 866.454.6010
Logistics/Ops: 866.454.6010
535 N. WW White Road
San Antonio, TX 78219
Sales: 800.284.0488
Logistics/Ops: 210.333.8112
142 Pine Haven Shores Rd.
Shelburne, VT 05482
Sales: 802.800.2540
Logistics/Ops: 802.985.2512
4700 Bethlehem Road,
Richmond, VA 23230
Sales: 804.201.2400
Logistics/Ops: 804.342.1161
4516 N Barker Road
Spokane Valley, WA 99027
Phone: 509.892.9420
Toll free: 800.728.6157
8365 N. 76th Street
Milwaukee, WI 53223
Sales: 800.356.9245
Logistics/Ops: 800.356.9245
312 S. Chester Street
Sparta, WI 54656
Sales: 800.362.5864
Logistics/Ops: 800.362.5864
899 Grossman Drive
Schofield, WI 54476
Sales: 800.472.0017
Logistics/Ops: 800.472.0017